


 русский
 Español
 中文简体
Industry News

Home / News / Industry News / What Makes Electric Warehousing Vehicle Instruments Reliable in Cold Storage and High-Vibration Fleets
What Makes Electric Warehousing Vehicle Instruments Reliable in Cold Storage and High-Vibration Fleets
Admin 2026-10-09Content
- 1 Why Standard Automotive Gauges Fail on the Warehouse Floor
- 2 Key Technical Specifications Procurement Teams Should Verify
- 3 Matching Instruments to Specific Vehicle Types
- 4 Cold Storage Compliance: A Case Study in Reliability
- 5 Customization Options for Fleet Managers
- 6 Common Mistakes When Specifying Warehouse Vehicle Instruments
- 7 Frequently Asked Questions About Warehouse Vehicle Instruments
- 7.0.1 Q1: Can these instruments work with both lithium and lead-acid batteries?
- 7.0.2 Q2: What is the operating voltage range for electric stacker instruments?
- 7.0.3 Q3: Do suppliers provide CAN protocol documentation for system integration?
- 7.0.4 Q4: How long should a pilot test run before a fleet-wide purchase?
Why Standard Automotive Gauges Fail on the Warehouse Floor
At six in the morning, a pallet stacker is pulled from the charging bay and driven into a chilled aisle held well below freezing. The operator turns the key, and the display takes almost a minute to respond. When it finally lights up, the battery bar is dim and flickers every time the forks lift. By mid-morning the truck has been parked, and the shift supervisor is looking for a replacement.
Scenes like this explain why buyers who search for electric warehousing vehicle instruments are rarely looking for a definition. Facility managers, fleet supervisors and product engineers want to know which display will keep working in a freezer, which one will survive daily jolts over dock plates, and which specifications actually matter when they compare suppliers. This guide answers those questions from the perspective of the people who have to keep trucks running every day.
Most instrument problems in warehouse vehicles do not appear on a datasheet. They show up as slow screens, fogged lenses, loose connectors and battery readings that cannot be trusted, and each of these leads to unplanned downtime.
The Hidden Cost of Instrument Failure in Cold Storage
A dead or unreadable gauge is often treated as a minor inconvenience, but its cost compounds quickly. Without a clear battery reading, operators either cut shifts short out of caution or push trucks until they stop in the middle of an aisle. Both outcomes are expensive. A stranded truck blocks traffic, delays picks and usually requires a recovery vehicle and a technician before the aisle can be cleared.
Cold storage adds problems that passenger-vehicle instruments were never designed to handle. Liquid crystal panels respond slowly at very low temperatures, and some drop to a nearly black image until they warm up. When a warm truck returns from the freezer to a dock at ambient temperature, moisture can condense on the inside of the lens, which makes the screen look hazy or patchy. The table below summarizes the most common patterns that maintenance teams report.
| Failure pattern | What the operator sees | Operational impact |
|---|---|---|
| Slow display response in freezer aisles | Blank screen for up to a minute | Delayed start and lost time at shift change |
| Condensation after cold-to-warm transfer | Hazy or streaked display | Battery level misread and early charging |
| Loose connector after repeated vibration | Intermittent reset or dead segments | Sudden loss of readout and possible drive fault |
| Voltage dip during heavy lift | Screen flicker or restart | Operator confusion and unscheduled stop |
The practical lesson is that cold-rated instruments must be specified as a system. The display module, the circuit board, the connectors and the housing all need to tolerate the same temperature range, and the enclosure must be designed so that condensation cannot sit on the optical surface. A display that performs well in a workshop test but fails on the route from freezer to dock has not really been tested for the job.
Vibration and Voltage Spikes in High-Throughput Material Handling
Electric stackers, walkie trucks and pallet jacks spend their working lives crossing uneven floor joints, dock plates and loading bridges. Each impact transfers energy into the instrument housing and the wiring harness. Over thousands of cycles, that energy can loosen crimped terminals, crack solder joints and gradually change the behavior of a display that once worked perfectly.
Electrical stress is equally important. The voltage of a traction battery falls as it discharges, and controllers, contactors and motor drives create short spikes whenever they switch. An instrument that depends on a narrow supply window will reset or misreport under these conditions. Designers therefore look for the following characteristics:
- A wide input voltage range that covers the full discharge curve of the battery pack as well as the charging voltage.
- Protection against reverse polarity, load dump events and transient spikes on the supply line.
- Mechanical mounting that isolates the display from vibration, combined with locking connectors rated for continuous movement.
When these three areas are handled well, the instrument becomes almost invisible in daily operation, which is exactly the goal in a high-throughput facility. Operators should never have to think about the gauge, because a gauge that demands attention is usually a gauge that is failing.
Key Technical Specifications Procurement Teams Should Verify
Technical sheets are often written to make products look comparable, but procurement teams gain far more by translating each parameter into an acceptance test. The sections below explain what each specification means in a warehouse and what evidence a supplier should provide to prove it. Used this way, a datasheet becomes a checklist that you can apply to every supplier on your shortlist.
Ingress Protection Beyond the Datasheet
The ingress protection code describes how well an enclosure resists solid objects and water. Two ratings appear most often in warehouse specifications. An IP65 enclosure is dust tight and resists low-pressure water jets from any direction, which covers normal rain and most light washdown. An IP67 enclosure is also dust tight and can tolerate temporary immersion at a limited depth, which gives a larger margin when crews clean trucks with pressurized hoses or when condensation pools around connectors.
A rating alone does not guarantee field performance. Ask suppliers which test standard was used, whether the rating applies to the display face or only to the housing, and how the gaskets perform after repeated temperature cycles. A sealed enclosure that is opened during service without proper reseating can lose its protection, so the connector design and the service procedure deserve attention as well. For buyers looking for an IP67 battery indicator for pallet stackers, the practical question is whether the seal remains intact after two years of washdown and freezer transfers.
| Rating | Dust protection | Water protection | Typical warehouse use |
|---|---|---|---|
| IP65 | Dust tight | Low-pressure jets from any direction | Dry indoor fleets and light outdoor use |
| IP67 | Dust tight | Temporary immersion at limited depth | Washdown areas, cold rooms and frequent cleaning |
CAN Bus Communication and Battery Management Integration
A display that only shows a battery bar is useful, but a display connected to the vehicle network over a CAN bus can do much more. It can read the state of charge, battery temperature, fault codes and operating mode directly from the battery management system or the motor controller. This allows the instrument to show estimates that reflect the actual condition of the pack, rather than a simple voltage reading that is distorted by load.
Integration is only as good as the documentation behind it. Before accepting a supplier's claim of CAN support, procurement teams should confirm the following points:
- The bit rate, frame format and termination requirements are documented and match the vehicle network.
- The message list is complete, including the identifiers for state of charge, fault codes and warnings.
- The instrument behaves safely when messages are missing, showing a clear communication fault rather than a false reading.
- A sample trace captured on a real controller is available for review before the first order is placed.
When these conditions are met, the operator sees a reliable estimate of remaining runtime, and the maintenance team can read fault history without opening the truck. That single capability often justifies the additional cost of a networked instrument within the first year of operation.
Display Readability Under Glare and Darkness
Warehouses are lit in very different ways. Cold white LED fixtures in freezers, high ceilings with reflective racking and the bright openings of loading doors all create glare at different points along a route. An instrument that is clear in a showroom can become unreadable when sunlight reaches the screen at a low angle, or when a freezer light reflects off the lens at the exact moment the operator looks down.
Two display technologies dominate this category. Segment displays are efficient, simple to read and well suited to a fixed set of symbols such as battery level, direction and warnings. Color TFT panels allow richer graphics, fault code text and multiple languages, but they demand more power and need higher brightness and anti-glare treatment to remain readable. The right choice depends on how much information the operator needs in the moment. A pallet stacker operator mainly needs battery level and a few warnings, while a reach truck operator may need height, steering angle and diagnostic messages on the same screen.
Ask for readability tests under the actual lighting of your facility. A display measured only in a laboratory may not reflect the reflections found on a dock or in a freezer aisle, and those reflections are what operators actually experience.
Matching Instruments to Specific Vehicle Types
Different electric trucks place different demands on their instruments. Mast height, travel speed, operator position and the amount of information required all change the best choice of display. Matching the instrument to the vehicle type is one of the most effective ways to reduce both cost and failure rates, because it prevents fleets from paying for features they will never use or, worse, buying a display that cannot cope with the environment.
| Vehicle type | Typical environment | Recommended display | Priority specification |
|---|---|---|---|
| Pallet jack | Short routes, low speed | Compact LED battery indicator | Simple, robust mounting |
| Pallet stacker | Cold rooms and dock transitions | Round or diamond LED level display | Sealed housing and wide voltage input |
| Walkie truck | Frequent vibration and washdown | Compact segment display | Vibration-resistant connectors |
| Reach truck | Tall racking and mixed lighting | Integrated round dashboard | CAN communication and fault codes |
| Order picker | Elevated work and frequent stops | Multi-zone color display | Readability and self-diagnosis |
Pallet Stackers and Walkie Trucks
These vehicles are compact, operated at low eye level and exposed to constant vibration from floor joints and uneven surfaces. The operator needs to see the battery level at a glance while walking beside the truck, so the display should be large enough to read from a short distance without requiring a head turn. A ten-segment LED bar is often the most intuitive format, because each segment represents a clear portion of the charge and operators learn to read it instantly, even when they are wearing gloves.
For these trucks, the enclosure rating and the mounting method matter more than advanced features. A sealed housing with a shallow profile reduces the chance of impact damage, while a firm mounting bracket keeps the display from resonating at the frequencies that cause connector fatigue. A useful test is to mount a sample on a truck and drive it over a known rough section of the facility for several weeks before committing to a large order.
Reach Trucks and Order Pickers
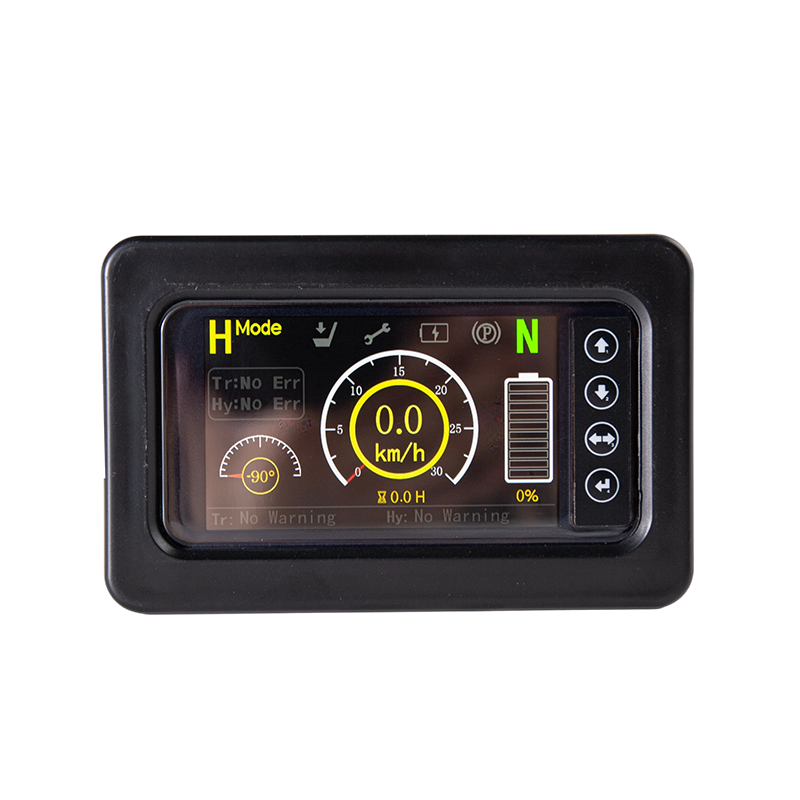
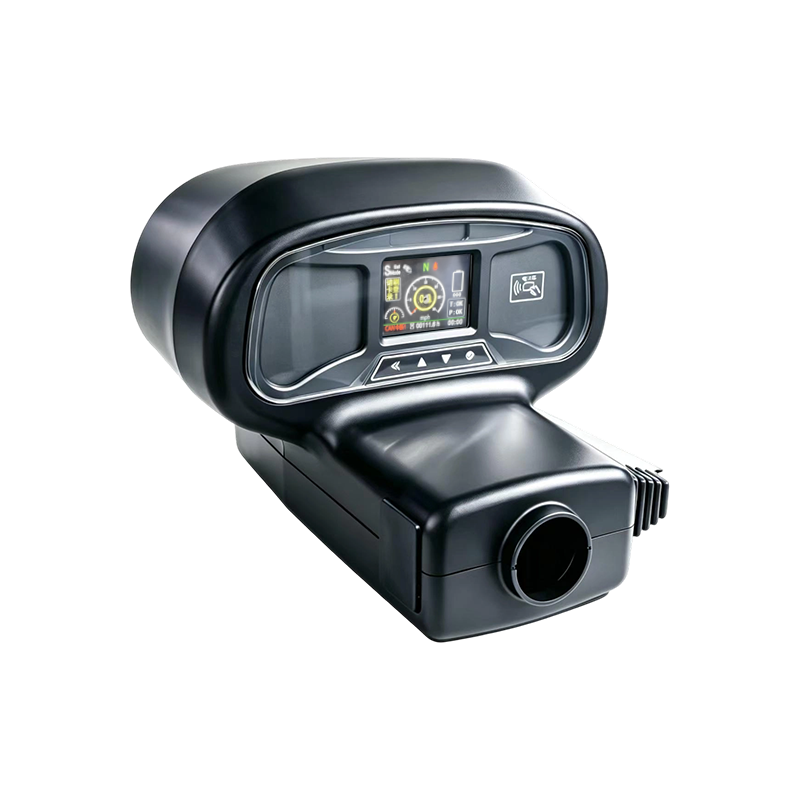
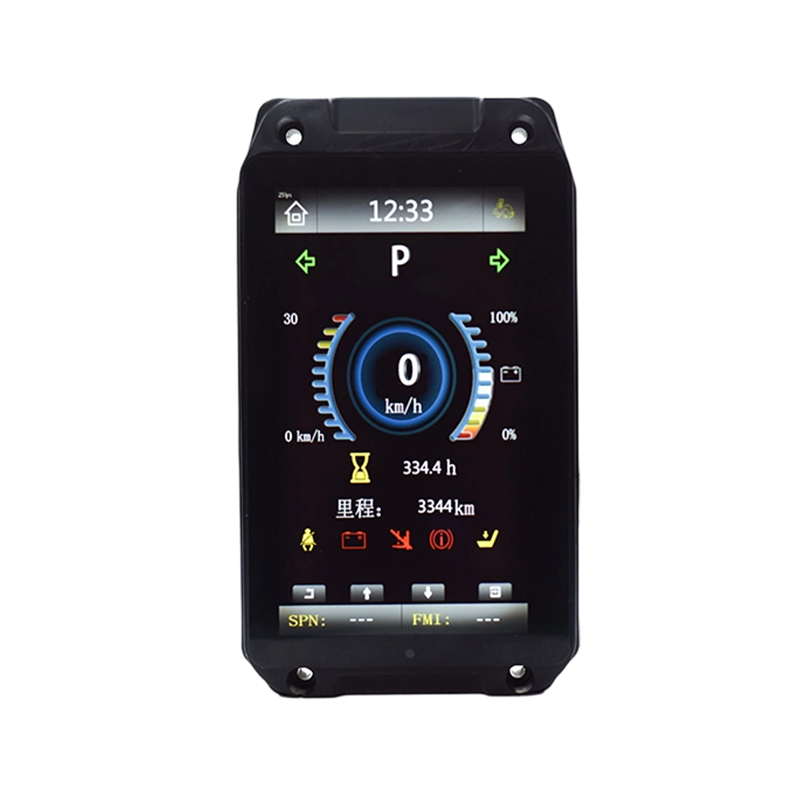
Reach trucks and order pickers operate at height and must monitor several parameters at once. The operator needs the battery state, the mast height, the steering angle and any warnings from the drive or lift systems. Information of this kind is best presented on a round or rectangular dashboard that combines a clear graphic display with indicators that can be read in a single glance.
Because these trucks often share data with the controller, CAN communication is a practical requirement rather than an optional extra. Self-diagnosis is equally valuable. When a fault occurs at height, the operator should see a short code and a plain description, which lets the maintenance team plan the repair before the truck returns to the ground. The illustration below shows how downtime might be distributed across subsystems in a typical fleet. The values are illustrative and intended to show how fault codes help teams focus their attention.
Reading this kind of breakdown helps teams decide where instrument features will have the largest effect. In many fleets, the display itself is not the primary cause of downtime, but a well-designed instrument reduces the time needed to identify and correct the problem, and that time is often the most expensive part of a failure.
Cold Storage Compliance: A Case Study in Reliability
A regional operator running more than one hundred electric stackers in a deep-freeze facility reported frequent display failures. The instruments worked well in a workshop, but in the freezer aisles, screens took too long to appear, and condensation formed on the lens whenever trucks returned to the dock. Operators began charging trucks early because they could not trust the battery reading, which reduced the number of available trucks during peak hours.
The operator worked with the supplier to redesign the requirements around the actual route. The main changes were the use of components rated for wide operating temperatures, conformal coating on the circuit boards to resist moisture, and a sealed lens assembly with a breathable membrane that equalizes pressure during temperature transitions without allowing water to enter. The team also added a short warm-up sequence so that the display reached full brightness before the operator began work.
After six months, the maintenance team reported that display-related downtime had fallen by roughly two thirds. The more important result was operational. Operators stopped charging trucks out of caution, and fleet availability during morning peaks improved noticeably. When buyers plan a similar project, the sequence below provides a reliable structure.
- Map the complete temperature profile of each route, including the transition zones at doors and dock plates.
- Specify the operating temperature range for the instrument as a system, not as a single component.
- Run a pilot on the coldest route for at least one full season before rolling out the design across the fleet.
- Record failure events with the time, temperature and vehicle identity so that patterns can be identified quickly.
Cold-zone reliability is rarely determined by one feature. It comes from consistent choices in components, sealing, coating and test procedures, which is why a field pilot is more informative than any single certificate.
Engineers who want to see how a cold storage instrument is validated can request the test plan and results for the relevant temperature range before committing to a project.
Customization Options for Fleet Managers
Standard instruments cover most applications, but fleets often have specific needs. A customer may want its own startup graphic, a particular connector layout to match an existing wiring harness, or a communication format that follows the protocol of a specific controller. Customization can reduce installation time, simplify operator training and keep the instrument consistent with the rest of the fleet's equipment.
- Startup screens and logos that reflect the facility or fleet identity, provided the file size and color depth suit the display.
- Connector arrangements and harness lengths that align with the mounting positions already used on the trucks.
- Message mapping that converts a controller's proprietary data into the display format required by the operator.
- Faceplate labels in the languages used by the workforce, with symbols that match local training materials.
The most useful starting point is the communication protocol used by the vehicle controller, together with a wiring diagram and a list of the parameters the operator must see. With this information, a supplier can outline a configuration and a sample build plan, and the fleet team can evaluate it before committing to volume.
Customization should always be documented. A written specification that records the message map, the connector pinout and the startup sequence makes future replacements simple, even if the original supplier is no longer involved. Documentation of this kind is also what allows a maintenance team to swap a failed unit in minutes rather than days.
Common Mistakes When Specifying Warehouse Vehicle Instruments
Experienced buyers still make errors when they move quickly from a catalog to a purchase order. Most of these mistakes are easy to avoid once they are recognized, and the list below captures the ones that appear most often in post-installation reviews.
- Specifying a voltage range based only on the nominal battery voltage, without considering the full discharge and charging range.
- Accepting an ingress rating without asking which test standard produced it or whether it applies to the complete assembly.
- Choosing a display format that looks attractive in a showroom but becomes unreadable under the reflections of a freezer aisle.
- Assuming that CAN support means full integration, when the message list and fault handling have never been verified on a real controller.
- Ordering in volume before a pilot unit has been tested on the coldest and roughest route in the facility.
A short acceptance checklist covering voltage, sealing, communication, readability and field testing prevents most of these problems. It also gives procurement, engineering and operations teams a common language when they compare suppliers, which shortens the decision cycle considerably.
Frequently Asked Questions About Warehouse Vehicle Instruments
Q1: Can these instruments work with both lithium and lead-acid batteries?
Yes, provided the instrument supports the full voltage range of both battery types and can read the state of charge through the correct method. Lithium packs typically provide state of charge through the battery management system over CAN, while lead-acid packs are often estimated from voltage and load. Buyers should confirm which method the instrument uses and whether it can be configured for the battery chemistry on each truck.
Q2: What is the operating voltage range for electric stacker instruments?
A wide input range of about 8 V to 100 V DC is a common requirement because it covers typical 12 V, 24 V, 36 V and 48 V traction systems, along with the transient spikes produced by controllers. The exact figure should be checked against the battery specification of each vehicle, including its maximum charging voltage.
Q3: Do suppliers provide CAN protocol documentation for system integration?
Reputable suppliers should provide a message list, bit rate, frame format, termination guidance and sample traces. Buyers should also ask whether the supplier offers integration support during the pilot phase, because the first installation on a real controller often reveals details that are not visible in any document.
Q4: How long should a pilot test run before a fleet-wide purchase?
A pilot should cover at least one full seasonal cycle when cold storage is involved. This allows the team to observe performance during the coldest months, the transition periods and the busiest operating hours. Records of failures, charging behavior and operator feedback provide the evidence needed to approve a larger order.
For exclusive deals and latest offers, sign up by entering your email address below.

CONTACT
- 88 Chuangye Street, Qingshanhu Street, Lin 'an District, Hangzhou City, Zhejiang, China
- fldz@fengletech.com
- +86-571-61097576
- +86-13721109386
- +86-15067105688
NEWSLETTER
Contact us today to get your exclusive solution and quote.
We promise never to disclose your privacy.
Copyright © Hangzhou Fengle Electronic Technology Co., Ltd. All Rights Reserved
Custom Forklift Electrical Parts Manufacturers
